For manufacturers, logistics giants and exporters, the risk of transportation damage is always present when protecting bulky or irregularly shaped goods. Scratched appliances, contaminated chemical barrels and broken beverage trays all mean huge financial losses and brand damage. Traditional rigid packaging boxes add weight and waste; standard packaging films lack toughness. PE heat shrinkable packaging provides a better solution that combines decades of advances in materials science to overcome these challenges. Dongguan Donghui Heat Shrinkable Film Co., Ltd. is a leading manufacturer and supplier of PE heat shrinkable packaging in China, with operations all over the world, which is a strong proof of the powerful functions of this technology. We use German automated extrusion processes and strict quality control to provide durable and adaptable packaging films to ensure the safety of goods from the factory to the final destination. Let's understand why PE shrink packaging is the smart and economical protective barrier needed by modern industry.
PE heat shrink packaging provides unmatched strength, adaptability and cost-effectiveness for the integration and protection of large items. Unlike fragile alternative materials, polyethylene (PE), especially blends of high density polyethylene (HDPE) and linear low density polyethylene (LLDPE), have good properties
Physical toughness: Our films have a tensile strength of over 18MPa, an elongation at break of over 500%, and have excellent puncture/tear resistance. This means that the film stretches rather than breaks when stressed, absorbing impact and resisting wear caused by moving cargo. The strapping remains intact and the corners are effectively protected.
Temperature tolerance: Operate perfectly in harsh environments (-20 ° C to 60°C). There will be no embrittlement due to low temperatures during frozen transportation; there will be no softening or sagging in high-temperature warehouses.
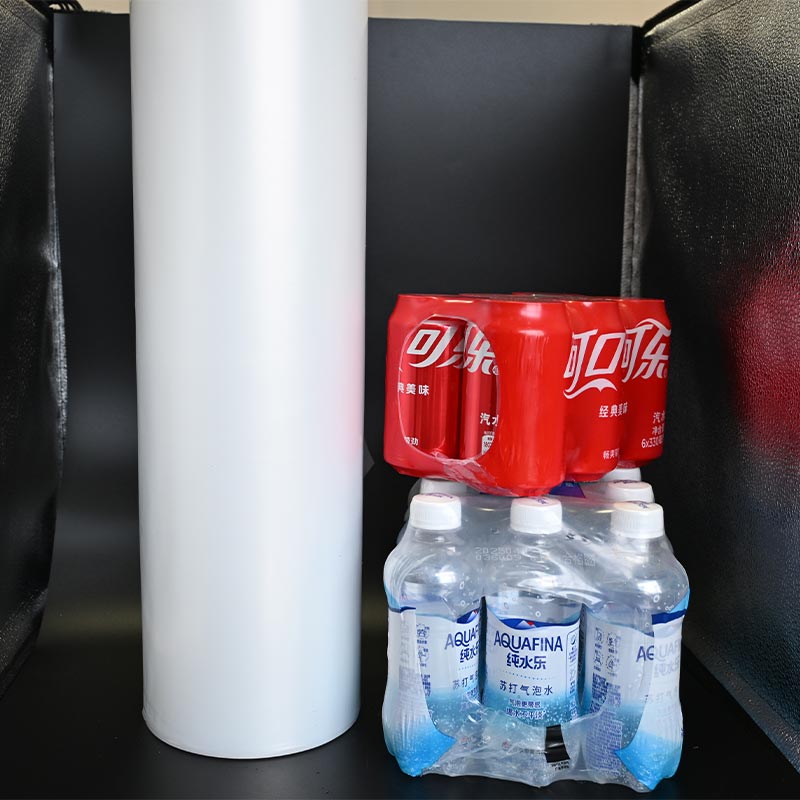
Best shrinkage performance: The precisely designed shrinkage rate of PE heat shrink packaging ensures rapid and uniform shrinkage at standard hot air tunnel temperatures. The film fits tightly to complex shapes without wrinkles or bubbles, fixing the contents without wasting material.
Food is safe and widely used: Strictly manufactured from HDPE/LLDPE that meets the GB4806 food grade standard to ensure no odor migration or pollution. This safety certification, coupled with its excellent physical properties, makes it ideal for industries such as beverage, packaged food and personal care product transportation.
Reduce costs and reduce waste: Ultra-thin thickness (0.02mm-0.15mm) minimizes the amount of material used per tray without sacrificing strength. Tight packaging reduces sliding damage, thereby reducing losses. Reduced packaging weight reduces transportation costs.
| Industry/Application | Donghui PE Film Advantage |
| Logistics / Warehousing(Pallets, Machinery Parts) | Exceptional puncture resistance protects against forks & shifting. Uniform shrink locks loads securely. |
| Beverage & Food (Water/Milk/Drink Multi-packs, Food Cases) | Food-safe material. High clarity options. Stretch absorbs bottle impacts. |
| Home Appliances (Washing Machines, Refrigerators, Ovens) | High tensile strength shields corners. Resists scuffs/scratches. Custom sizes cover XL items. |
| Chemical & Daily Essentials (Detergent Drums, Bottle Cases) | High chemical resistance. Excellent seal integrity protects contents. Stable against leaks & vapors. |
| Export / International Shipping | Low-temp performance suits reefer containers. Certifications meet EU/US standards (RoHS, FDA). |
| Sustainability Priority | >90% Recyclable PE content. Lightweighting reduces CO2 footprint. Green Supply Chain Certificate. |
Our PE heat shrinkable packaging films are specially designed to have a wide temperature range. They maintain excellent flexibility, tensile strength and puncture resistance over a wide operating temperature range of-20 ° C to +60 ° C. This means that even in severe cold weather, trays bundled with our films will not experience brittle cracking during transfer from freezer to transportation. Similarly, exposure to temperatures as high as 60°C will not cause the film to prematurely soften, deform or reduce its load-bearing capacity.
Yes, polyethylene (PE) itself is recyclable. The core advantage of our PE heat shrink packaging lies in its material composition: the main ingredients are a blend of HDPE and LLDPE. These are recognized recyclable resins. Donghui prioritizes this, and specific measures include:
Use materials with a recyclability of more than 90%.
Holding green supply chain assessment certification reflects our commitment to the environment.
Comply with RoHS and FDA environmental/health standards.
Encourage the use of thin films (as low as 0.02 mm) to reduce material consumption per tray.
Custom printing is carried out with environmentally friendly water-based inks. Although recyclability depends on the ability of local infrastructure to separate clean PE films from mixed waste streams, Donghui ensures the recyclability of basic materials. We actively support industry progress to improve closed-loop recycling solutions for polyethylene films.
Traditional tray stretch wrap films often sacrifice strength to increase stretchability, while our PE heat shrink packaging provides a stronger protective barrier, and its key characteristics to prevent tearing and punctures include:
Excellent tensile strength: Much higher than standard tensile films, and it is not easy to break even at high tensile strength.
Excellent puncture and tear resistance: Designed to withstand sharp corners of home appliances, staples on cartons, and the impact of forklifts or moving goods.
High elongation: While maintaining extremely high strength, the film can stretch significantly before breaking, effectively absorbing impact energy and being difficult to pierce.
Shrink fit: After shrinking, the film can wrap the item tightly, significantly reducing internal movement, thereby avoiding abrasion and piercing of the film itself.