In the bottled water industry, packaging quality directly influences transportation safety, shelf appeal, product stability, and customer satisfaction. PE heat shrink film has become one of the most trusted packaging materials for bottled water manufacturers because it offers strong bundling performance, excellent transparency, cost efficiency, and superior protection during logistics. This article explores everything buyers, distributors, and manufacturers need to know about bottled water packaging PE heat shrink film, including benefits, material selection, production considerations, common customer pain points, and industry trends.

Bottled water packaging PE heat shrink film is widely used for bundling bottled water products due to its flexibility, durability, puncture resistance, and high shrink performance. Businesses in the beverage industry rely on this packaging solution to improve transportation efficiency, reduce packaging damage, and enhance visual presentation on retail shelves. In this guide, you will learn how PE shrink film works, its advantages over alternative packaging materials, how to select the right film thickness, and what factors affect packaging quality and production costs.
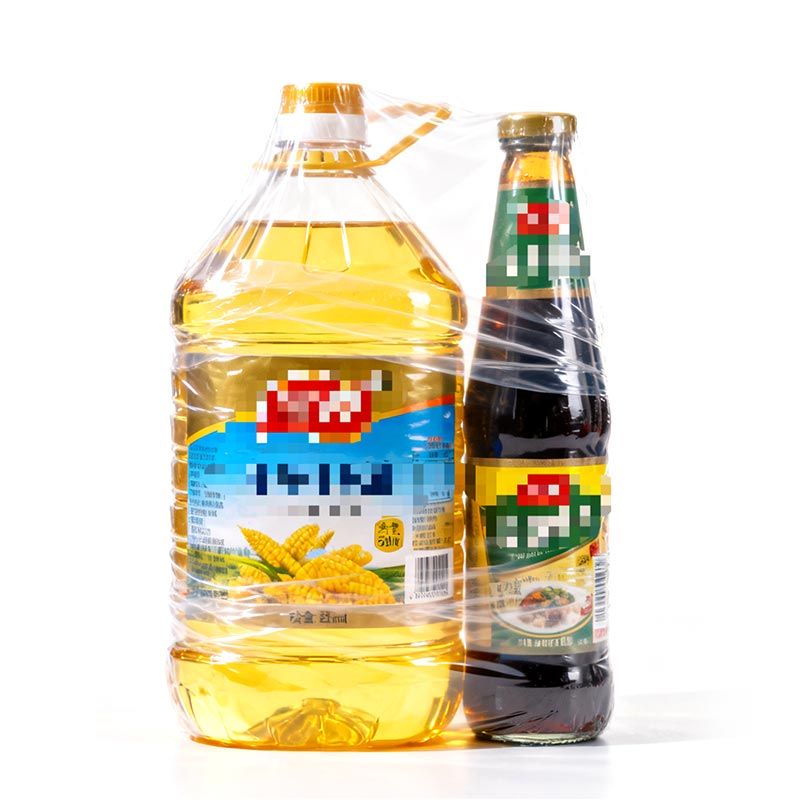
PE heat shrink film is a polyethylene-based plastic film designed to tightly wrap products when heat is applied. In the bottled water industry, it is commonly used to bundle multiple bottles together for transportation, storage, and retail display.
When exposed to controlled heat inside a shrink tunnel or heating machine, the film contracts evenly around the bottles, creating a secure and compact package. This process improves handling efficiency while protecting products from dust, moisture, and movement during shipping.
The most common materials used include:
The bottled water industry requires packaging materials that can withstand demanding logistics conditions. Water bottles are heavy, slippery, and often stacked during transportation. PE heat shrink film addresses these challenges effectively.
| Benefit | Description |
|---|---|
| Strong Load Stability | Keeps multiple bottles tightly bundled together during transport. |
| Cost Efficiency | Uses less material compared to rigid packaging alternatives. |
| Excellent Transparency | Allows product labels and branding to remain visible. |
| Moisture Resistance | Protects products from water and humidity exposure. |
| High Flexibility | Suitable for different bottle shapes and packaging sizes. |
Manufacturers prefer PE shrink film because it supports automated high-speed packaging lines while maintaining reliable packaging integrity.
Several important features determine the quality and performance of bottled water packaging film.
Premium PE shrink film maintains stability even under changing warehouse temperatures and rough handling conditions.
For bottled water producers, packaging failure can result in damaged products, leakage, customer complaints, and increased logistics costs. Therefore, film quality directly impacts operational efficiency.
The shrink packaging process is relatively straightforward but highly effective.
| Step | Process Description |
|---|---|
| Product Arrangement | Bottles are grouped into bundles. |
| Film Wrapping | PE film surrounds the bottle bundle. |
| Heat Application | Heat tunnel activates shrink properties. |
| Cooling | Film cools and tightly secures the bottles. |
The film’s molecular structure reacts to heat by contracting evenly around the products, producing a secure package that minimizes movement and improves stability.
Many beverage manufacturers encounter recurring packaging issues that affect productivity and product quality.
Low-quality shrink film often causes unstable packaging, especially when transporting large-volume bottled water products over long distances.
High-quality PE shrink film offers several advantages that directly solve packaging problems.
| Packaging Challenge | PE Shrink Film Solution |
|---|---|
| Bottle movement during transport | Strong shrink force stabilizes products. |
| Film breakage | Enhanced puncture resistance improves durability. |
| High packaging cost | Optimized thickness reduces material usage. |
| Poor shelf appearance | Smooth shrink performance improves presentation. |
| Warehouse humidity | Moisture-resistant structure protects bottles. |
Modern PE shrink film technology also supports high-speed automatic packaging lines, reducing labor requirements and increasing production efficiency.
Different packaging applications require different film structures.
| Film Type | Main Characteristics |
|---|---|
| Single Wound Film | Suitable for automatic packaging systems. |
| Center Folded Film | Provides efficient wrapping for bundled products. |
| Printed Shrink Film | Enhances brand visibility and product marketing. |
| Heavy-Duty Shrink Film | Ideal for large bottled water packs. |
Heavy bottled water packages typically require thicker and stronger film grades to ensure safe transportation.
Selecting the correct film thickness is critical for packaging performance and cost control.
| Film Thickness | Typical Application |
|---|---|
| 30-40 Microns | Lightweight beverage packaging. |
| 40-60 Microns | Standard bottled water bundles. |
| 60-100 Microns | Heavy-duty transportation packaging. |
Factors to consider when selecting film thickness include:
A balanced combination of strength and material efficiency helps reduce operational costs while maintaining packaging safety.
| Packaging Material | Advantages | Limitations |
|---|---|---|
| PE Shrink Film | Flexible, strong, cost-effective | Requires heat application |
| Carton Packaging | Good protection | Higher material cost |
| Stretch Film | Simple application | Lower visual appeal |
| Rigid Plastic Crates | Reusable | Expensive and bulky |
PE shrink film remains one of the most economical and efficient solutions for bottled water packaging worldwide.
Buyers should evaluate several technical indicators before purchasing PE shrink film.
Consistent film quality ensures smooth operation on automatic packaging machinery and reduces downtime caused by packaging defects.
PE heat shrink film is manufactured using advanced extrusion and cooling technologies.
| Production Stage | Description |
|---|---|
| Raw Material Mixing | Polyethylene resins are blended. |
| Film Extrusion | Molten plastic is formed into film. |
| Cooling Process | Film structure is stabilized. |
| Stretching | Creates shrink memory effect. |
| Winding | Finished film is rolled for shipment. |
Advanced manufacturing technology improves film uniformity, shrink consistency, and overall durability.
Although widely used for bottled water packaging, PE shrink film is also suitable for many other industries.
Its versatility makes it one of the most widely used packaging materials across global manufacturing industries.
Environmental concerns are driving innovation in packaging materials. Modern PE shrink film manufacturers are developing more sustainable solutions while maintaining strong packaging performance.
Many companies are now focusing on balancing packaging durability with environmental responsibility.
Choosing the right supplier is essential for long-term packaging stability and business growth.
A reliable supplier should provide:
Working with an experienced manufacturer helps reduce packaging risks and ensures compatibility with different packaging machines and production requirements.
PE heat shrink film is mainly used to securely bundle bottled water products together for transportation, storage, and retail display.
Yes. Heavy-duty PE shrink film is specifically designed for large and heavy beverage bundles with high puncture resistance and strong load stability.
Yes. Manufacturers can customize thickness, width, printing, shrink ratio, and roll size according to customer requirements.
Common causes include insufficient film thickness, poor material quality, improper shrink temperature, and excessive product weight.
Many PE shrink films are recyclable depending on local recycling systems and material composition.
Using high-quality shrink film with automatic packaging systems can significantly improve production speed and reduce packaging failures.
Bottled water packaging PE heat shrink film has become an indispensable packaging solution for modern beverage manufacturers. Its combination of durability, flexibility, cost efficiency, and strong protective performance makes it ideal for demanding transportation and retail environments.
As packaging technology continues to evolve, businesses are increasingly focusing on stronger, lighter, and more sustainable shrink film solutions. Choosing the right packaging material not only protects products but also improves logistics efficiency, enhances shelf presentation, and supports long-term business growth.
Whether you are a bottled water producer, distributor, wholesaler, or packaging equipment supplier, understanding the performance and application of PE heat shrink film is essential for maintaining product quality and operational efficiency in today’s competitive beverage market.
Dongguang County Donghui Heat Shrink Film Co., Ltd specializes in reliable and high-performance PE heat shrink film solutions for bottled water packaging and beverage industries worldwide.
Our experienced team provides customized packaging solutions designed to improve packaging efficiency, transportation safety, and product presentation.
Contact us today to discuss your packaging requirements and discover professional PE shrink film solutions tailored to your business needs.